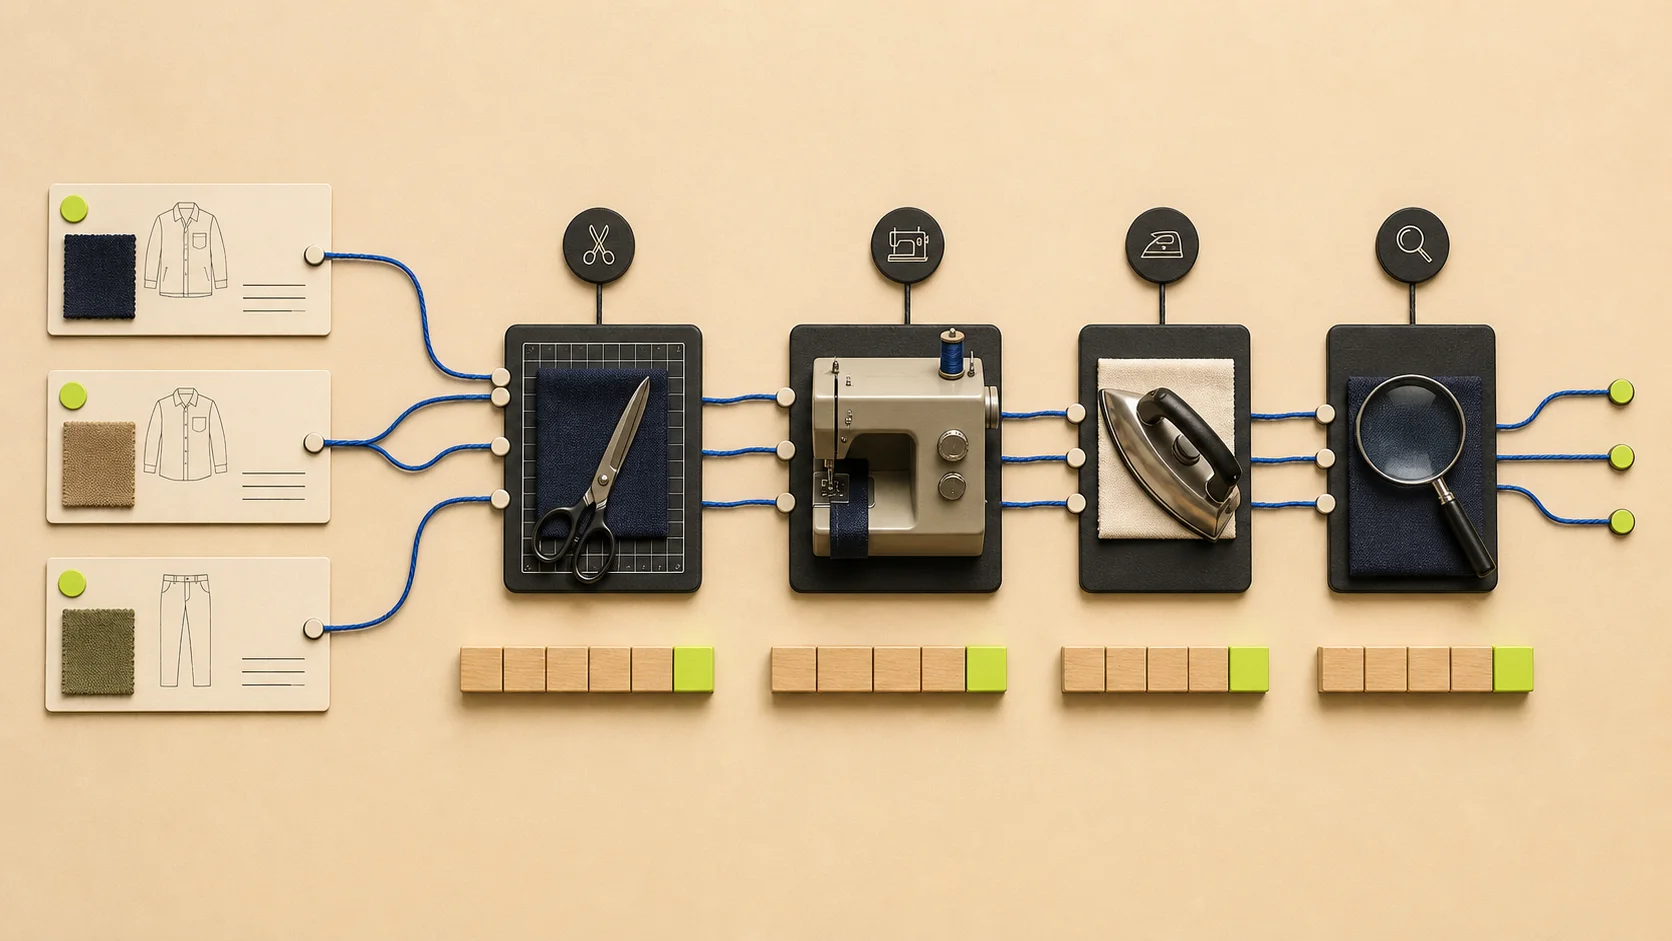
A short run does not mean a simple schedule. Three styles can compete for the same cutting table, sewing capability, finishing station, quality check, fabric delivery, and people. A late trim can make an apparently efficient sequence impossible. A fabric or construction change can turn a familiar operation into a longer one.
AI can predict durations, cluster similar jobs, or suggest a revised sequence. The schedule still has to satisfy physical precedence, capacity, material, quality, safety, and due-date constraints. The first goal is not intelligence. It is feasibility.
Build the digital routing before the optimization
For each order, record:
- style, variant, quantity, release date, due date, and priority reason;
- required material and trim status;
- operation sequence and allowed alternatives;
- machine, tool, fixture, skill, and workstation requirements;
- standard time and uncertainty range;
- setup and changeover time based on the previous job;
- batch, curing, washing, drying, inspection, and transport delays;
- quality gates, rework route, and expected failure rate;
- shift calendar, planned maintenance, and safe capacity;
- outside-process lead times and confirmation state.
Do not let a model treat a missing duration as zero or an unavailable specialist as a generic resource. A schedule can be mathematically tidy and physically impossible.
Separate precedence from capacity
Google’s job-shop example explains two basic constraints. Tasks within a job must follow their required order, and one machine cannot process overlapping tasks. It then minimizes makespan, the total length of the schedule.
Apparel adds detail. Cutting must precede sewing, but different sewing operations may require different machines or skills. Finishing can depend on completed batches. An outside dye process introduces transport and a separate provider calendar. Quality failure can send an item backward.
The objective also matters. Minimizing makespan may not minimize late orders, overtime, changeovers, work in process, or disruption to a priority sample. A planner needs to know what the system optimized and what it did not.
A transparent three-style baseline
FashionMember created a fictional routing file at content/data/FM-030-short-run-operations.csv. It includes three styles—TOP-C, DRE-B, and JKT-A—moving through cutting, sewing, finishing, and quality check with different durations and due days.
The reproducible scripts/fm030-short-run-schedule.php orders styles by earliest due date and schedules each operation as soon as both the style and machine are available. The result is feasible under the narrow rules supplied:
- TOP-C completes on day 5 against a day-8 due date.
- DRE-B completes on day 10 against a day-10 due date.
- JKT-A completes on day 15 against a day-12 due date.
- Total makespan is 15 days.
The three-day lateness for JKT-A is not a bug to hide. It tells the planner that the assumed capacity and sequence cannot meet every due date under this heuristic. The next questions are operational: can work overlap differently, is another qualified sewing resource available, can a due date move, can a batch split safely, or is the order mix infeasible?
The script is not an AI model and does not claim optimality. It omits changeovers, people, material arrivals, rework, batching, maintenance, uncertainty, and outside processes.
Give AI three bounded roles
1. Estimate with ranges
AI or statistical models can estimate operation times from style attributes, quantity, material, construction, operator or line history, and observed conditions. Report a distribution or interval, not only an average. New construction and small samples need wider uncertainty.
Use time-based validation. Compare estimates with actual completion at operation level and look for systematic underestimation by material, factory, style complexity, or worker group. Do not use the model to create unrealistic labor standards or penalize people for variation outside their control.
2. Search feasible sequences
OR-Tools’ scheduling overview describes assigning tasks to limited resources under constraints. Optimization can explore far more sequences than a planner can manually enumerate, but the output is only as credible as the routing, capacity, and objective.
Apparel research reflects that complexity. A 2021 scheduling and rescheduling decision-support study modeled release times, sequence-dependent setups, blocking, resource constraints, and stochastic processing times. Its reported case results belong to that studied environment; they are evidence that richer constraints matter, not a guaranteed result for another factory.
3. Detect changes and propose a response
Use current events—material receipt, machine outage, quality hold, absence, revised order, completed quantity—to flag that the approved schedule no longer matches reality. Generate alternatives with explicit impact: which order becomes late, how much overtime or transfer is required, and which assumption changed.
Do not let the system silently rewrite the production promise. A named planner approves the revised plan and records why.
Plan for demand uncertainty and tail loss
Production quantity and timing depend on demand that may be wrong. A robust fashion-apparel planning study uses Conditional Value at Risk to consider production cost and tardiness under demand uncertainty across plants. Its specific model and case are not a template for every small run, but they make a useful point: average outcomes can conceal expensive tail scenarios.
For a small label, test at least:
- material arriving two or five days late;
- operation time 20 percent above estimate;
- rework on a quality-sensitive step;
- a priority sample inserted midweek;
- one key machine or outside process unavailable;
- demand below plan, leaving finished units with no order;
- demand above plan, requiring a second run.
The planner should see which commitments survive each scenario.
Keep human capacity and safety outside the optimization bargain
A model can reduce a schedule by assuming continuous capacity that people cannot safely deliver. Working time, breaks, skill limits, training, ergonomic needs, maintenance, and legal requirements are constraints—not optional penalties the solver can buy through overtime.
OSHA’s sewing eTool notes musculoskeletal risks associated with sewing stations, fine work, scissor work, and material handling and offers example ergonomic solutions. The resource is guidance and does not create new requirements, but it reinforces why a schedule should not treat every available hour as interchangeable capacity.
Ask workers and line leaders whether the routing reflects actual practice. Provide a way to flag unsafe or impossible assignments without punishment.
Measure the deployed planning system
Compare the AI-assisted schedule with the current process and a simple baseline. Track:
- on-time completion and total tardiness;
- makespan and work in process;
- setup and changeover time;
- overtime, idle time, and expediting;
- material-related delays;
- quality failures and rework;
- schedule revisions and percentage actually executed;
- planner overrides and reasons;
- worker-reported feasibility and safety issues;
- forecast and duration calibration.
A plan that looks efficient but is repeatedly ignored is not an operational success.
Limits of the scheduling exercise
The worked schedule is a fictional earliest-due-date baseline with one machine per operation type and deterministic durations. It is not a live manufacturer model, staffing plan, labor standard, or production recommendation. Real deployment requires manufacturer, production, quality, worker, safety, finance, and customer-commitment review.
Sources and verification
- Google OR-Tools: Job shop problem — precedence, machine exclusivity, feasible schedules, and makespan.
- Google OR-Tools: Scheduling overview — official scheduling problem and resource-allocation guidance.
- Robust Production Planning in Fashion Apparel Industry under Demand Uncertainty — primary research on cost, tardiness, plants, and demand uncertainty.
- A Scheduling and Rescheduling Decision Support System for Apparel Manufacturing — primary research on apparel constraints and rescheduling.
- OSHA sewing and related procedures eTool — official ergonomic risk and solution guidance.
content/data/FM-030-short-run-operations.csvandscripts/fm030-short-run-schedule.php— FashionMember’s fictional, reproducible baseline executed August 31, 2026.
How this story was checked
- Sources
- 5 linked records · View list
- Last verified
- Reporting desk
- FashionMember AI & Retail Desk
- Format
- Analysis
- AI assistance
- Used with editorial review; disclosed above.